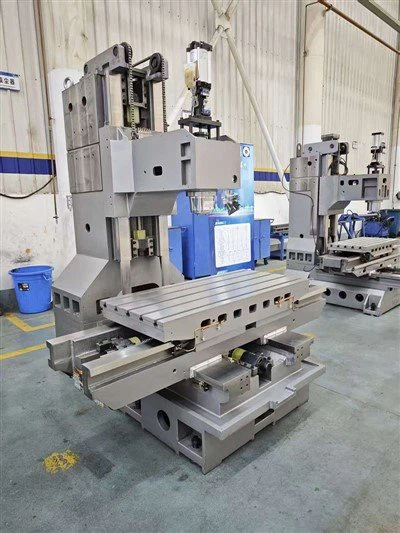
If you’ve ever held a well-machined aluminum part—say, a sleek aerospace bracket, a custom component for high-end automotive performance, or a precision part for medical device assembly—you know that its surface quality isn’t just a cosmetic detail. It’s a critical performance factor: a rough, uneven surface can cause premature wear, interfere with tight tolerances, trap contaminants, or even compromise structural integrity. As an aluminum CNC machine supplier, I’ve worked with shops of all sizes—from small job shops to large manufacturing facilities—and the question I hear most often is: “How do we consistently improve the surface quality of our machined aluminum parts on a CNC machine?” Aluminum Cnc Machine
Let me start with a truth I’ve learned over 12 years in this industry: there’s no magic trick here. Surface quality is the sum of dozens of small, intentional choices, from the tool you pick to how you set up your machine, how you cut, and even how you prepare your raw aluminum stock. I’ve seen shops pour tens of thousands of dollars into high-end CNC machines only to get mediocre finishes because they skipped the basics, and I’ve seen a shop with a well-used 3-axis mill producing mirror-like parts just by tweaking their process step by step. If you’re ready to stop guessing and start getting consistently better surface quality on your aluminum CNC parts, this is the breakdown of what actually works, from a supplier who’s watched these changes play out in real production.
First, let’s talk about something that’s way more important than most new operators realize: your raw aluminum stock. Too often, shops grab the cheapest 6061 or 7075 aluminum bar off the shelf and wonder why their finishes are inconsistent. Not all aluminum is created equal for machining. For example, 7075 is a high-strength alloy commonly used in aerospace, but it’s prone to built-up edge (BUE)—that gunk of tiny aluminum chips that welds to the cutting tool’s edge mid-cut, leaving scratch marks and a rough surface—if you don’t work with the right grade or pre-treat it properly. Even something as simple as how your stock was extruded can make a difference: extruded bar that’s been properly stress-relieved after extrusion is far less likely to deform during machining, which means you don’t end up with uneven cuts that create rough spots or dimensional errors. I always tell customers that spending an extra 5-10% on quality, stress-relieved raw aluminum is a no-brainer, especially for parts with tight surface requirements. I’ve had customers come back to me after switching from cheap local stock to the consistent, certified aluminum we supply for our recommended setups, reporting that their scrap rates from surface quality issues dropped by 40% in the first month. That’s not a small number.
Next up: your cutting tools. This is where a lot of shops waste money on fancy tools that aren’t right for aluminum. Aluminum is a soft, ductile metal, which means it doesn’t cut like steel—your go-to tool for machining steel will likely give you terrible results on aluminum. Let’s break this down. First, tool material: carbide tools are standard for aluminum, but not all carbides are equal. Look for carbide grades engineered specifically for non-ferrous metals, with a fine grain structure—this gives the tool edge the sharpness it needs to cut aluminum cleanly without BUE. Coating matters too. A lot of shops use TiN (titanium nitride) coatings for general machining, but for aluminum, you want something with low friction to prevent BUE. Diamond-like carbon (DLC) coatings are ideal here; they’re smooth, non-stick, and reduce chip adhesion dramatically. I’ve seen a shop switch from uncoated carbide end mills to DLC-coated ones on a 6061 aluminum job, and their surface finish went from Ra 3.2 micrometers (which is decent but not great) to Ra 0.8 micrometers, almost mirror-like, in one setup.
Then there’s tool geometry. For face milling, use a high-positive rake angle—this means the cutting edge is angled forward, which shears aluminum instead of forcing it, reducing heat and BUE. For profile milling, a corner radius end mill (also called a ball nose or bull nose, depending on the radius) is better than a square end mill if you’re working with complex surfaces, because it creates smoother transitions between cuts. Also, never use a dull tool—this should go without saying, but I see it all the time. A dull edge doesn’t cut; it tears the aluminum, leaving micro-scratches and a rough surface. When you notice the finish starting to degrade, or the tool taking longer to cut, replace it immediately. Don’t wait until you scrap a whole batch of parts.
Now, let’s talk about the biggest variable most people overlook: cutting parameters. Speed, feed rate, and depth of cut aren’t just about getting parts done fast—they’re the core of surface quality. For aluminum, you need to balance these three to avoid BUE, heat buildup, and tool vibration. Let’s start with spindle speed. Aluminum has a low melting point, so running too slow is bad because it makes the tool rub instead of cut, generating heat that softens the aluminum and makes it stick to the tool. But running too fast can also cause issues, especially with small tools that can’t handle the centrifugal force, leading to tool deflection and uneven cuts. A good rule of thumb for 6061 aluminum with a 10mm DLC-coated carbide end mill is a spindle speed of around 1500-2000 RPM, with a feed rate of 0.15-0.2 mm per tooth. Adjust for tool size: smaller tools (like 3mm end mills) can go as high as 5000 RPM, while larger 20mm tools might top out at 1200 RPM.
Depth of cut is another key factor. When doing roughing, you can take deeper cuts to remove material quickly, but for finishing passes (the last cut that gives you the surface quality), you need to make the depth of cut as small as possible—usually between 0.1mm and 0.5mm. A light finishing pass means the tool is only removing a tiny layer of material, so it can cut cleanly without tearing or leaving marks. Also, climb milling vs. conventional milling: climb milling (where the tool rotates in the same direction as the feed) is almost always better for aluminum. It reduces BUE because the tool cuts into the chip instead of pushing against it, lowers heat, and leaves a smoother surface. Conventional milling is more likely to cause the tool to pull the workpiece slightly, leading to chatter marks—those rhythmic spiral lines you see on rough surfaces that no one wants.
Coolant and lubrication might seem like a small detail, but they make a huge difference in preventing BUE and reducing heat. I can’t tell you how many shops I’ve visited that run their CNC mill dry for aluminum. Dry machining generates way too much heat, which softens the aluminum and causes chips to weld to the tool edge. For most aluminum machining, a synthetic coolant with high lubricity is ideal—look for one formulated for non-ferrous metals, with a concentration of around 5-10%. Mist cooling works too for operations where flood coolant is hard to direct, but flood cooling is better for heavy cuts and finishing passes because it keeps the tool and workpiece consistently cool. One tip I always share: direct your coolant directly at the cutting zone, not just the workpiece surface. If the coolant isn’t hitting the edge of the tool where it’s cutting, it’s not doing its job.
Next, setup and fixturing. Vibration is the enemy of good surface quality, and bad fixturing is the main cause of vibration during machining. If your aluminum part isn’t held rigidly, it will flex slightly when the tool makes a cut, leading to uneven cuts, chatter, and rough surfaces. Even a tiny amount of flex can ruin a finish, especially on thin-walled parts or parts with complex geometries. What’s the solution? First, use as many clamps or vises as possible to distribute pressure evenly, avoiding clamping near the cut zone if possible. For parts with thin walls, use custom soft jaws that match the part’s profile, or use a support fixture like a collet chuck or a vacuum fixture to hold the part without deforming it. Also, make sure your CNC machine is properly calibrated—check that the spindle is running true (no runout), that the axes are aligned, and that the work offset is set correctly. A machine with even 0.01mm of spindle runout can cause a tool to cut unevenly, leaving rough spots on every part. I always recommend a monthly calibration check for shops running high-precision parts; it takes an hour and prevents a lot of avoidable scrap.
Then there’s finishing operations, and no, I don’t mean just buffing after machining (though that can help for some applications). The final machining step, called a finish pass, is where you can really elevate the surface quality. A lot of shops make the mistake of rushing the finish pass, using the same feed and speed as roughing. Instead, for the finish pass, slow down the feed rate a little (try 0.1mm per tooth or lower) and run the spindle at the higher end of your speed range. For profile milling, use a climb milling finish pass, and make sure the tool is long enough to reach the cut but not so long that it flexes. Another trick for complex surfaces: use ball nose end mills with smaller stepovers between passes. A stepover of 10% of the tool diameter (instead of 20%) will leave smaller scallops between cuts, resulting in a much smoother surface that requires less post-machining work.
And let’s talk about post-machining steps, because they’re often the final touch that makes a good surface great. For parts that need a mirror-like finish, light hand polishing with a fine-grit sandpaper (1000 grit or higher) followed by a polishing compound can remove any micro-scratches left by machining. For parts that will be anodized, a smooth machined surface will take anodization more evenly, resulting in a consistent, attractive finish. I always recommend testing post-machining steps on a scrap part before doing it on production parts, because you don’t want to accidentally alter the part’s dimensions or surface roughness in a way that affects its function.
Now, I know what you’re thinking: this is a lot of small changes, and it’s easy to miss one. That’s why a systematic approach works best. When you’re working on improving surface quality, change one variable at a time, test it, and see what works for your specific parts and machine. Don’t swap out tools and change cutting parameters on the same day—you won’t know which change made the difference. Over the years, I’ve helped dozens of shops work through this process, and the ones that get the best results are the ones that track every change, document their setup, and don’t get frustrated when a tweak doesn’t work. Surface quality is a process, not a one-time fix.
At the end of the day, improving the surface quality of machined aluminum parts on a CNC machine isn’t about having the most expensive machine or the fanciest tools. It’s about understanding how aluminum behaves, paying attention to the details that affect cut quality, and refining your process step by step. If you’re looking to implement these changes in your shop, or if you have specific challenges with a particular aluminum alloy or part design, I’m here to help. Whether you need guidance on tool selection, CNC setup, or cutting parameters tailored to your production, our team can work with you to find the right solution for your needs. Reach out to our team to discuss your aluminum CNC machining projects and how we can support your goals for consistent, high-quality parts.
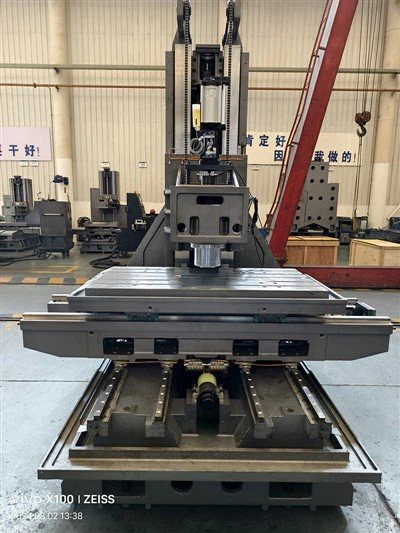
Horizontal Machining Center Frame References:
- Gillespie, L. K. (1999). Surface Finish Technology in Manufacturing. Society of Manufacturing Engineers.
- Shaw, M. C. (2005). Metal Cutting Principles (2nd ed.). Oxford University Press.
- Dimiduk, D. M., & Levy, M. (Eds.). (2001). Aluminum Alloys: Contemporary Research and Applications. Elsevier.
- Kalpakjian, S., & Schmid, S. R. (2014). Manufacturing Processes for Engineering Materials (7th ed.). Pearson.
- DeGarmo, E. P., Black, J. T., & Kohser, R. A. (2011). Materials and Processes in Manufacturing (11th ed.). Wiley.
Smartech Machinery & Equipment Co., Ltd.
As one of the most professional aluminum cnc machinemachine manufacturers and suppliers in China, we also support customized service. Please rest assured to buy bulk aluminum cnc machinemachine made in China here from our factory. Contact us for more details.
Address: Room 2832, Changping Commercial Mansion, Shihua Road, Futian Free Trade Zone, Shenzhen, China
E-mail: smartech@smartechcnc.cn
WebSite: https://www.smartech-cnc.com/
